See detailed overview, process notes, and recommendations for this industry use-case. For matching spares or machine selection, request a quick quote.
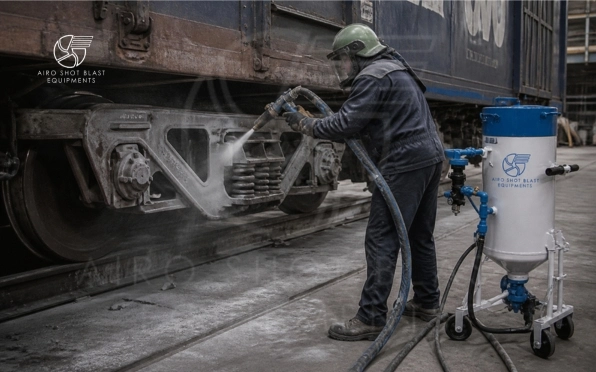
Shot blasting for railways and peening are essential to the construction and renovation of railroads since everything from wheels to entire carriages need to be cleaned or have their surfaces improved. Shot blasting equipment (air or wheel blast) offers remarkable productivity together with consistent quality as compared to manual working with power instruments.
There is a solution that works whether you're peening springs or cleaning new railway lines, processing a lot of small parts or just a few big ones. Here is a list of typical applications and cutting-edge tools that can handle them.
Descale brand-new tracks as they leave the factory and clean worn ones in preparation for further processes like profile regrinding or milling using shot blasting is most effective. Roller conveyor wheel blast machines, either as stand-alone equipment or integrated into a larger production line, quickly clean rails in a continuous feed-through process.
Shot blasting is widely used to clean a variety of objects, including carriage frames, bogie bolsters, helical springs, leaf springs, cylinder liners, manganese steel crossings, whole coaches before painting, etc.
We have provided more than 20 pieces of equipment for a variety of applications to railway workshops. Prior to hard chrome plating, the cylinders are shot blasted from the interior with aluminum oxide to remove corrosion, scale, and even out each surface.
Coil shot peening machines are widely used by the railway to shot peen coil springs that range in diameter from 70 mm to 450 mm (2.5" to 18"). Shot peening occurs on 6 to 8 coils per minute. To extend the fatigue life of components, shot peening is also used on leaf springs, helical springs, gears, and pinions.
Prior to painting, a newly constructed rail coach measuring 24 to 27 meters long and including the underside is cleaned in 3 to 4 hours using 16-wheel shot blasting equipment. Previously, cleaning the air blast room required 16 to 20 hours.
On a rail coach, shot blasting essentially extends the paint's lifespan. Numerous studies have demonstrated that the bond strength between the paint and the basic surface has a major role in how long the paint lasts. Prior to painting, mill scale, rust, and other pollutants must be completely and thoroughly removed. Additionally, a uniformly etched surface is necessary to ensure the quality of this bond.
Common production scenarios where shot blasting delivers the best finish, adhesion and throughput.
Pre-paint / Powder-coat prep
Remove mill scale and create a controlled profile for strong coating adhesion (Sa 2.5 / Sa 3).
Anti-corrosion surface cleaning
Uniform blast cleaning for steel plates, beams and fabricated structures before primer / epoxy.
Structural & fabrication lines
High-throughput processing on conveyor / roller lines with consistent finish and repeatable output.
Weld seam / scale removal
Clean weld areas, edges and heat-affected zones to improve coating quality and inspection readiness.
Deburring & edge rounding
Remove burrs and sharp edges on components for safer handling and better downstream fit-up.
Single-pass finish targets
Optimized media + wheel setup to achieve full cleaning in one pass with predictable surface profile.
A practical flow used on production lines to consistently hit Sa 2.5 / Sa 3 targets with the right profile.
Machines we quote for this job. Send size, material and finish — we will confirm the fit.
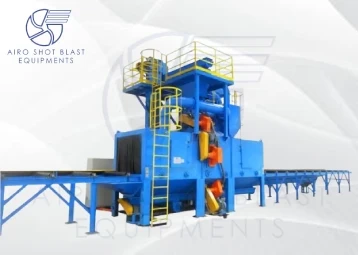
Roller conveyor shot blasting machine
| Product | Roller Conveyor Shot Blasting Machine |
|---|---|
| Machine Type | Roller Conveyor |
| Grade | Semi-Automatic |
| Pressure | 6-7 Bar |
| Number Of Doors | One |
| Power | 420 Volt |
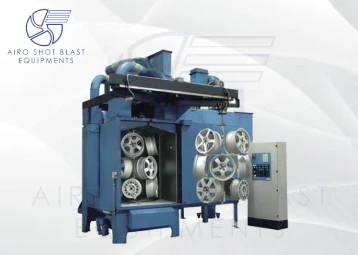
The wheel blasting machine is a powerful surface treatment equipment imp...
| Product | Wheel Blasting Machine |
|---|---|
| Material | MS Steel |
| Grade | Semi-automatic |
| Power | 3 HP |
| Capacity | 200 KG |
| Number of Door | Single Door |
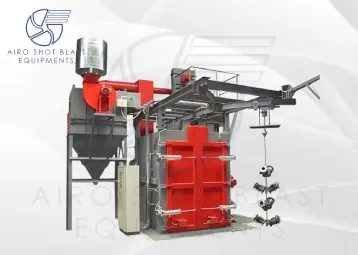
Airless hanger shot blasting machine type with a variable number of blas...
| Product | Hanger Shot Blasting Machine |
|---|---|
| Machine Type | Hanger Type |
| Automatic Grade | Automatic, Semi-Automatic |
| Number Of Doors | Double Door |
| Blast Wheel Size | 15 ½ x 2 ½ inch |
| Blast Wheel No. | 2 Nos. |
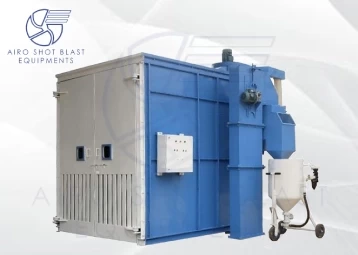
When compared to open-air blasting, the controlled environment of a shot...
| Material | Mild Steel |
|---|---|
| Motor Power | 10 Hp |
| Machine Type | Automatic, Manual |
| Cleaning rate | 3-5 sqr. mtr/ hr |
| Frequency | 50 Hz |
| Voltage | 415 V |
Typical ranges for roller conveyor blasting lines. Final specs depend on job size, wheel count and finish target.
| Parameter | Typical value / range |
|---|---|
| Cleanliness standard | Sa 2.5 (standard) / Sa 3 (on request) |
| Throughput | 500–3000 kg/hr (depends on section size, rust grade & line speed) |
| Surface profile | Rz 40–70 µm (achieved by shot/grit mix and wheel parameters) |
| Blast wheels | 4–8 units (coverage on all 4 sides, depending on chamber design) |
| Throwing speed | 70–80 m/s (wheel dependent) |
| Abrasive recovery | Floor screw conveyor → elevator → separator → recirculation to wheels |
| Dust collection | Pulse-jet dust collector (fine dust capture; clean air return) |
| Primer window | Ideally within 4 hours after blasting (site conditions may vary) |
Plant RFQ
Name, plant and machine type are enough. An engineer replies from the factory.